en
 de
 jp
 kor
 fra
 spa
 ru
 pt
 it
Surface Finishing Options for MIM Parts (Polishing, Plating, Passivation)
Surface Finishing Options for MIM Parts: Polishing, Plating, Passivation Complete Engineering Guide
Choosing suitable finishing options not only improves visual aesthetics, but also directly influences wear resistance, sealing performance, corrosion resistance and assembly reliability. Over‑specifying high‑grade surface treatment will raise production cost and lead‑time unnecessarily. This article explains core concepts of MIM surface quality, mainstream finishing processes including polishing, passivation and plating, process comparison, risk points, design guidance and manufacturing expertise from Harbermetal.
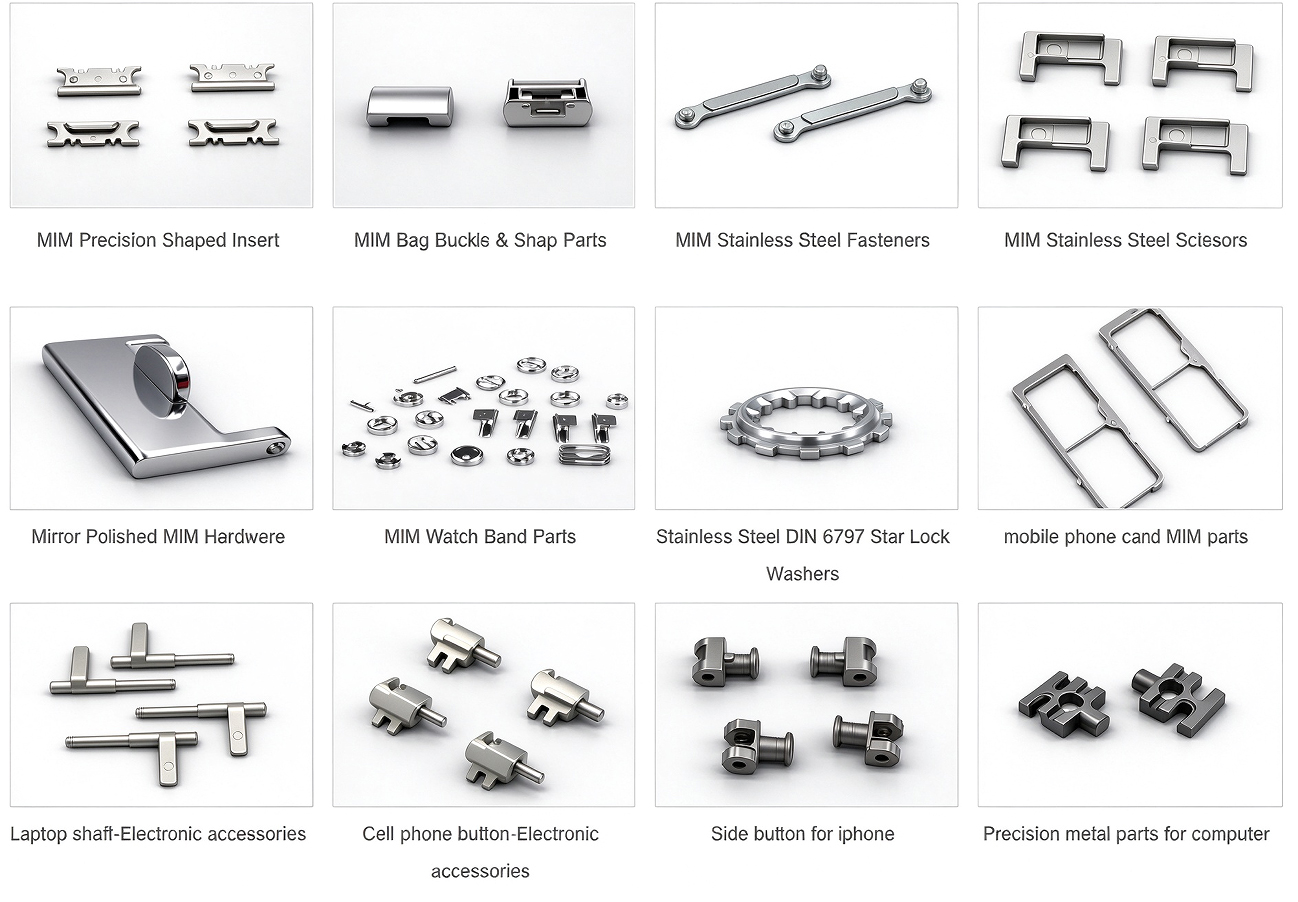
What Is Surface Roughness & Surface Finish for MIM Parts
Why Surface Finishing Matters for MIM Components
Improve wear performance: Smoother surfaces reduce friction coefficient for sliding mating parts and extend component service life.
Boost corrosion resistance: Proper passivation or sealing treatment blocks corrosive media from penetrating surface pores.
Meet cosmetic requirements: Consumer‑facing MIM hardware needs uniform, defect‑free visual appearance.
Guarantee coating adhesion: A clean, low‑roughness base surface is the precondition for reliable plating and PVD coating.
Eliminate sharp burrs: Deburr and round sharp edges to avoid stress concentration and assembly injury.
Mainstream Surface‑Finishing Processes for MIM Parts
1. Polishing (Mass Tumbling, Vibratory Finishing, Electropolishing, Mechanical Polishing)
Tumbling / Vibratory finishing: Batch mass finishing for deburring and edge radiusing. Achieves Ra 0.4‑1.2 μm. Ideal for high‑volume small‑size MIM hardware. Risk: Abrasive media may round fine sharp features.
Electropolishing: Electrochemical smoothing process, widely used for stainless‑steel MIM. Can reach Ra 0.1‑0.4 μm. Excellent for medical‑auxiliary and wearable‑device components. Can reveal subsurface pores if density is insufficient.
Mechanical polishing: Produces mirror‑grade high‑gloss surfaces (Ra 0.05‑0.2 μm). Higher cost, mainly applied for small‑batch decorative parts.
Key note: Polishing cannot fix internal porosity; low‑density MIM parts may show pin‑hole‑like pore openings after polishing.
2. Passivation
Typical use: Industrial hardware, non‑implant medical auxiliary MIM parts.
Advantages: No dimensional change, low extra cost, compatible with mass‑batch processing.
Limitation: Passivation cannot repair large open pores; parts with severe interconnected porosity will still suffer corrosion under salt‑spray conditions.
3. Plating & Coating Treatments
Electroplating / Electroless Nickel Plating: Provides corrosion protection, conductive surface or decorative appearance. Electroless nickel delivers uniform coating thickness even for complex internal cavities. Critical risk: Open surface pores trap plating solution, leading to blistering and peeling over time. High‑density MIM or pre‑sealing treatment is strongly recommended before plating.
PVD Coating (TiN, TiCN, DLC): Ultra‑thin hard‑coating layer for improving wear resistance. Minimal dimensional impact. Requires very clean, smooth base surface; surface defects will be amplified after coating. Suitable for high‑friction latch, gear and wearable decorative MIM components.
Other Common Auxiliary Finishing
Bead blasting: Creates uniform matte texture; frequently used as pre‑treatment step prior to coating.
Ultrasonic cleaning: Mandatory pre‑processing step to remove oil, residual binder and polishing debris before passivation or plating.
MIM Surface‑Finishing Process Comparison Table
| Finishing Process | Typical Ra (μm) | Main Purpose | Key Risk Points | Relative Cost |
|---|---|---|---|---|
| As‑Sintered | 0.8‑1.6 | Internal functional structural parts | Gate marks, minor sinter discoloration | Baseline (1.0×) |
| Tumbling / Vibratory Finishing | 0.4‑1.2 | Deburr, edge rounding | Fine feature rounding | 1.1‑1.25× |
| Electropolishing | 0.1‑0.4 | Smooth stainless‑steel surfaces, medical‑grade finish | Pore exposure for low‑density blanks | 1.3‑2.0× |
| Passivation | 0.8‑1.6 | Improve stainless‑steel corrosion resistance | Ineffective for high‑porosity parts | 1.05‑1.15× |
| Electroless Nickel Plating | 0.2‑0.8 | Wear & corrosion protection, decoration | Pore‑trapped chemical causing blistering | 1.4‑2.0× |
| PVD Coating | 0.1‑0.6 | High‑wear‑resistance thin hard coating | Base‑surface defects become visible | 1.6‑2.2× |
Critical DFM & Specification Tips for MIM Surface Finishing
Clarify whether the requirement targets functional performance or purely cosmetic appearance. Non‑visible internal components can keep cost‑effective as‑sintered + passivation finish.
High‑grade polishing / plating requires high sintered density (≥96‑97 % theoretical density). Evaluate density requirement at DFM review phase.
Be aware finishing may slightly alter sharp edges and tiny feature dimensions; reserve proper tolerance allowance.
Avoid specifying over‑demanding cosmetic standards for surfaces covered by assembly housings.
Define acceptance samples, Ra value, salt‑spray requirements and defect criteria on drawings before quotation.
Harbermetal: Your Trusted Metal Injection Molding Partner In China
Creative promotion copy: Many engineers copy CNC surface‑finish specifications directly onto MIM drawings, ignoring MIM’s inherent micro‑porosity risks. This results in polishing pinholes, plating blisters and unexpected rework costs. You don’t need to waste sampling budgets caused by mismatched surface‑treatment expectations. Send your 2D/3D drawings plus surface‑roughness, corrosion and cosmetic requirements to Harbermetal. Our engineering team carries out pre‑tooling DFM surface‑quality assessment, identifies porosity‑related finishing risks, and recommends the most cost‑effective finishing workflow before mold investment.
Optimizing Surface Quality in mim Machining: Harbermetal’s Expertise in Roughness and Finishing
Contact informationEmail: sales@harber‑mim.comTel: +86 0769‑82389116